
When production schedules tighten, retail promotions ramp up, or seasonal demand spikes unexpectedly, the last thing your team needs is a packaging issue slowing things down.
Cardboard boxes play an important role beyond simply holding a product. Packaging needs to protect what’s inside, work efficiently on packing lines, perform through distribution networks, and arrive at its destination in excellent condition. For FMCG businesses, those factors can have a direct impact on efficiency, stock availability and customer satisfaction.
At Abbe, we work with food, beverage and other FMCG businesses across Australia to develop corrugated solutions tailored to their products, fulfilment processes and supply chain needs.
Key Takeaways
- Effective transport packaging starts with understanding the product, handling conditions and the logistics journey.
- Clear forecasting and communication help maintain supply continuity during seasonal peaks and promotional periods.
- Structural design influences protection, pallet efficiency and ease of handling throughout distribution.
- Australian manufacturing and in-house design support more responsive collaboration and practical problem solving.
What is the purpose of corrugated packaging in FMCG operations?
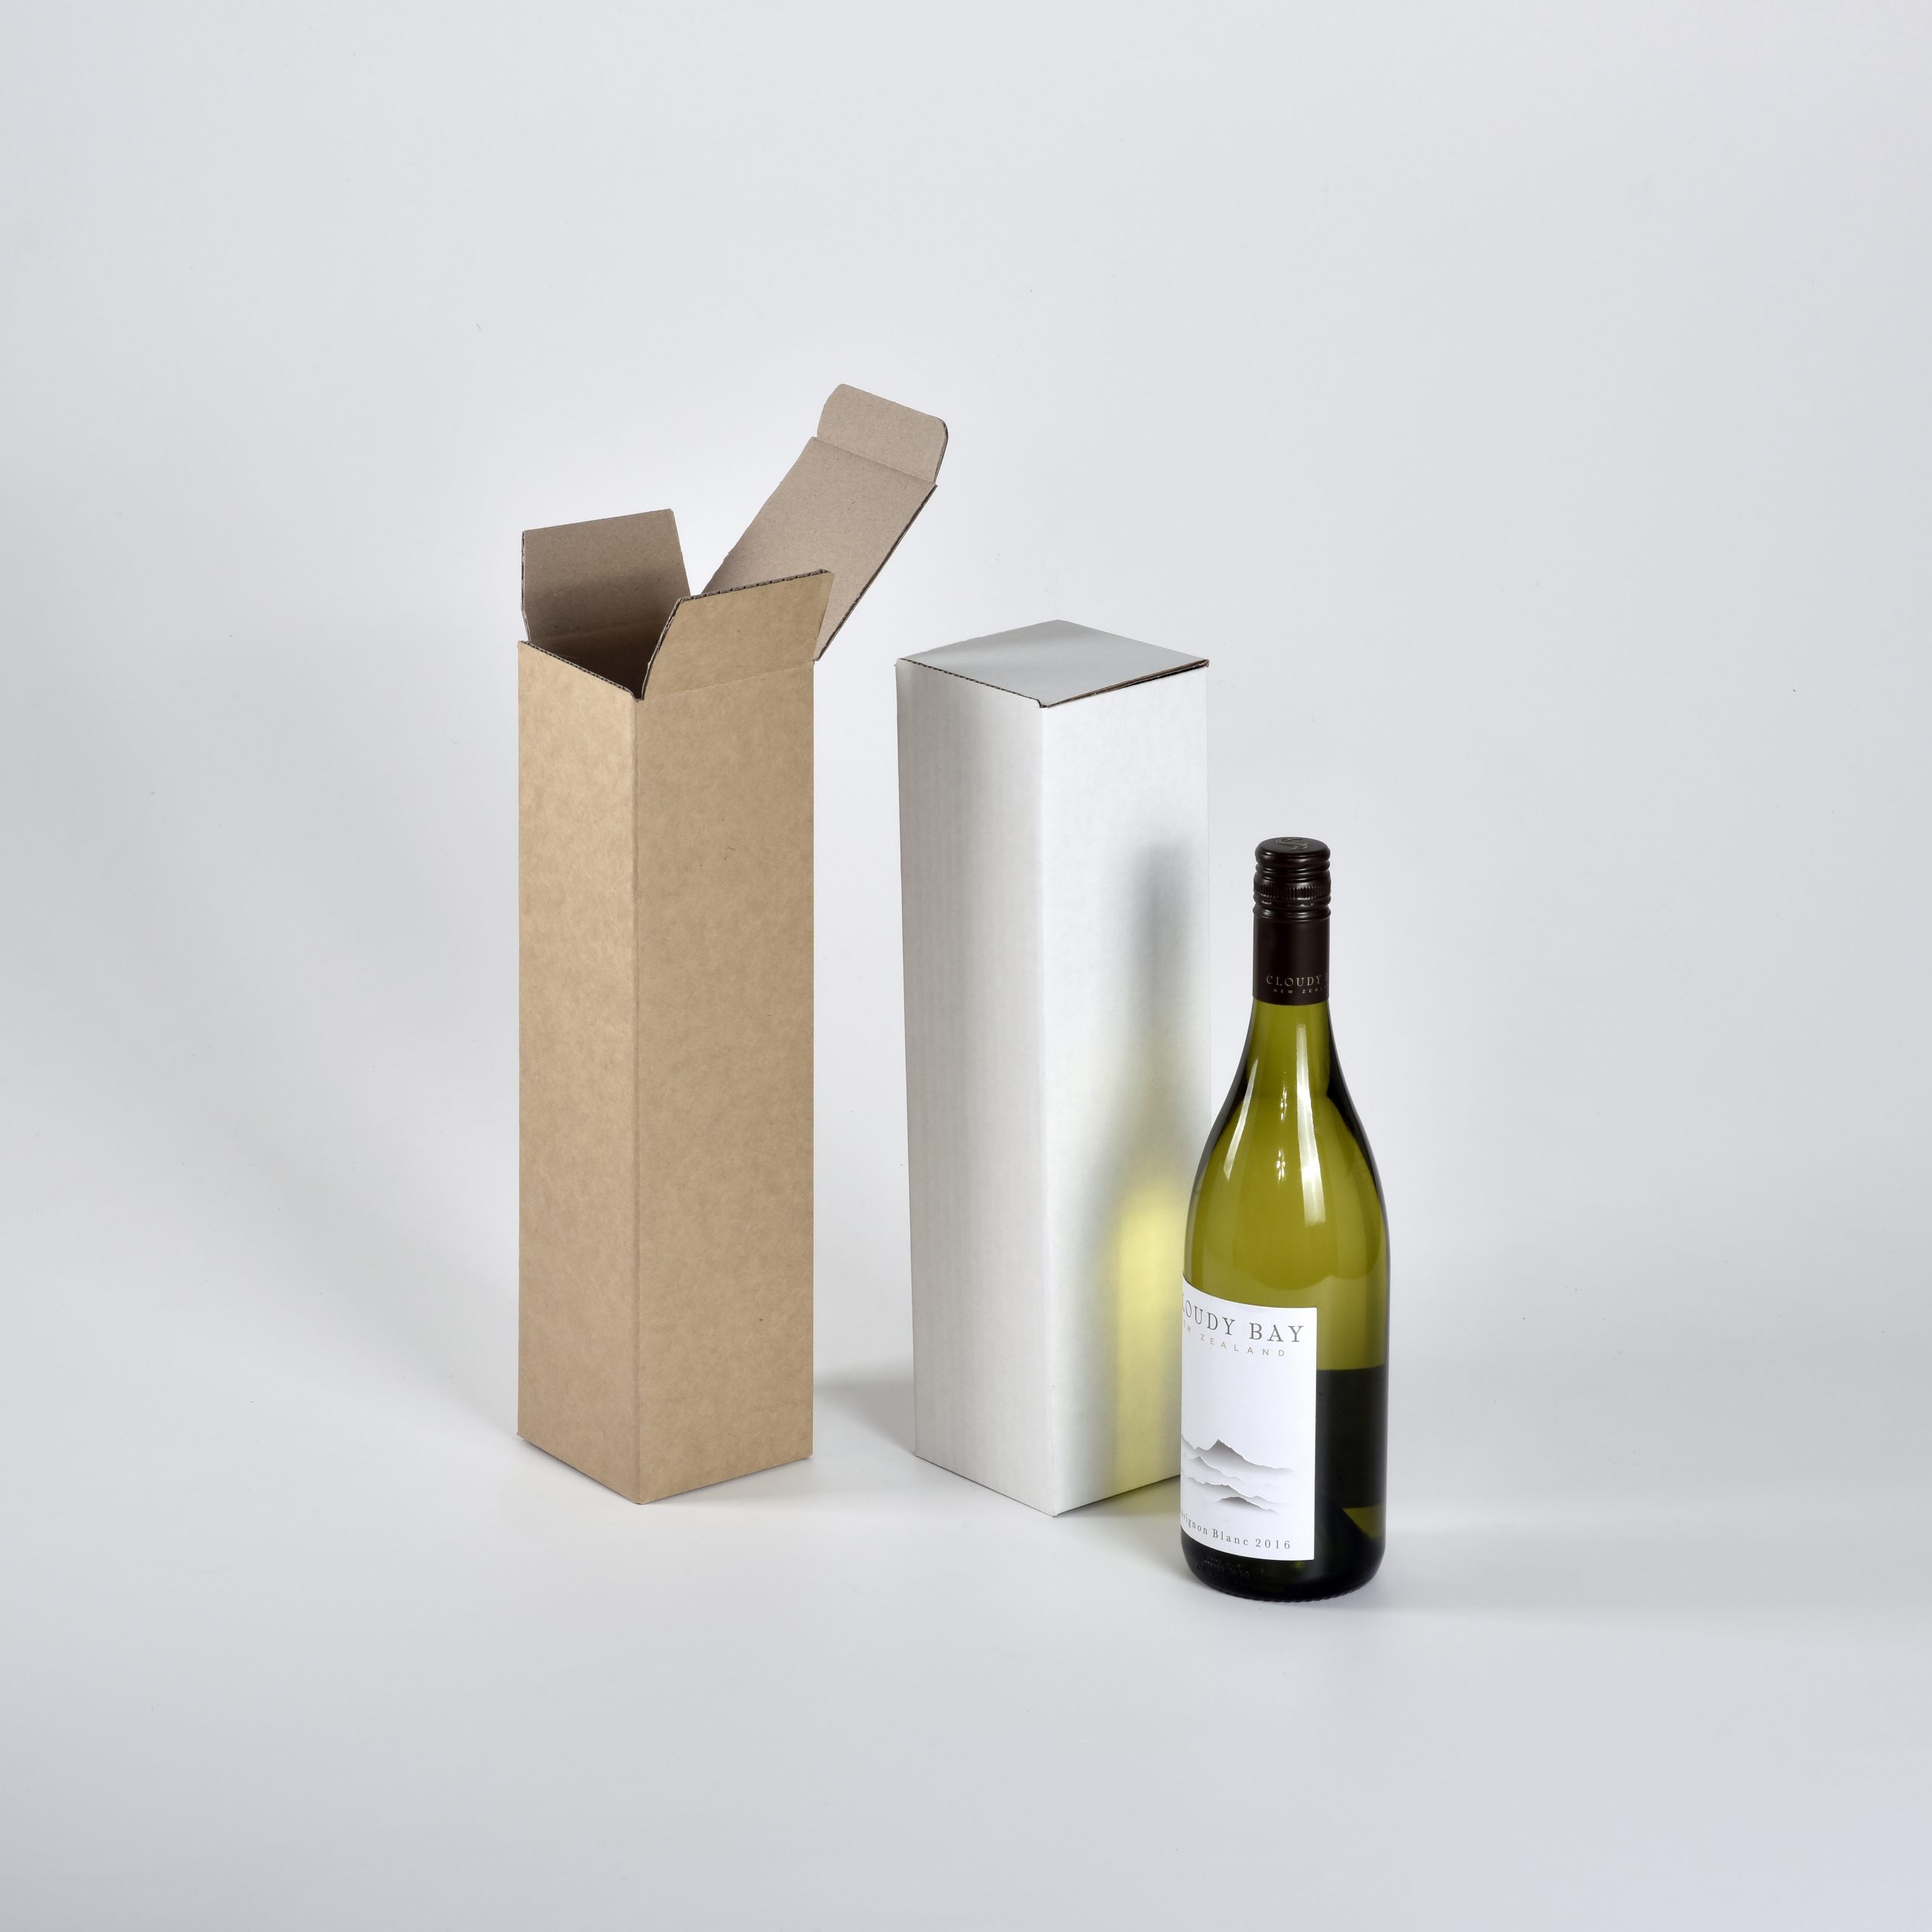
Corrugated board helps safeguard products from the packing line through to the retail shelf. Its layered construction provides strength while remaining lightweight, making it suitable for a wide range of consumer goods.
However, there is no one-size-fits-all solution.
A beverage multipack and a box of chocolate bars need corrugated packaging solutions tailored to their distinct supply chain demands. Product weight, stacking pressure, humidity, retail presentation and transport conditions can significantly influence the most suitable specification.
The best place to start isn’t simply with dimensions. It’s with understanding how an item is packed, stored, transported and displayed.
How can FMCG brands avoid packaging shortages?
The best results come from planning ahead and maintaining alignment across teams
While repeat orders can usually move through production quickly, new packaging formats often require additional steps such as design development, sample testing, artwork approvals and production scheduling before manufacturing can begin.
By understanding sales forecasts, promotional activity and expected seasonal demand early, manufacturers can plan capacity more effectively and reduce the risk of delays. When both parties are aligned, it’s much easier to respond to unexpected changes in demand.
How does structural design improve product safety?
Effective packaging protection relies on more than just selecting the right board grade. Structural design, product fit, weight distribution and stacking requirements all play an important role in how corrugated packaging performs throughout a supply chain.
At Abbe, packaging solutions are developed around the specific product, considering its size, weight, handling requirements and distribution environment. Depending on the application, this may involve regular slotted cartons, die-cut designs, protective inserts or divider systems.
By assessing how products will be stored, transported and handled before production begins, potential risks can be identified early, helping prevent costly damage or performance issues later.
What is shelf-ready packaging?
Shelf-ready packaging is designed to move directly from transport and storage into a retail display environment with minimal handling.
The challenge is balancing strength during transit with presentation in store.
Successful retail-ready formats typically consider:
- Product visibility
- Ease of opening
- Branding placement
- Shelf dimensions
- Replenishment efficiency
When these elements work together, retailers spend less time restocking and consumers can more easily find products on shelf.
How does packaging affect warehouse productivity?
Even the strongest corrugated packaging can cause problems if it’s difficult or time-consuming to use. The best solutions protect products while also supporting efficient packing and fulfilment operations.
Businesses looking to automate their operations may also benefit from right-sized packaging solutions that reduce waste and streamline packing processes.
For online orders, packaging often needs to withstand the demands of parcel delivery networks, requiring different solutions from those used in supermarket or retail distribution
What information should be included in a packaging brief?
A strong project brief helps manufacturers understand both product needs and operational objectives.
Useful information includes:
- Product dimensions
- Packed weight
- Storage conditions
- Forecast volumes
- Distribution methods
- Retail requirements
- Artwork expectations
- Packing processes
Sharing examples of existing formats, transit damage or handling challenges can also provide valuable context during development.
The more information available upfront, the easier it becomes to recommend an efficient and commercially practical solution.
Why FMCG Businesses Work with Abbe
At Abbe, we understand that successful packaging is about more than just the box itself. It’s about how products move through the supply chain, where potential challenges exist, and what the packaging needs to achieve at every stage.
That’s why our team takes the time to understand each customer’s product, operations and distribution requirements before recommending a solution. Whether the priority is product protection, packing efficiency, sustainability or retail presentation, we work collaboratively to develop packaging that supports those goals.
By combining local manufacturing with practical design and engineering expertise, we help businesses implement solutions that not only perform in the real world but also support long-term operational success.